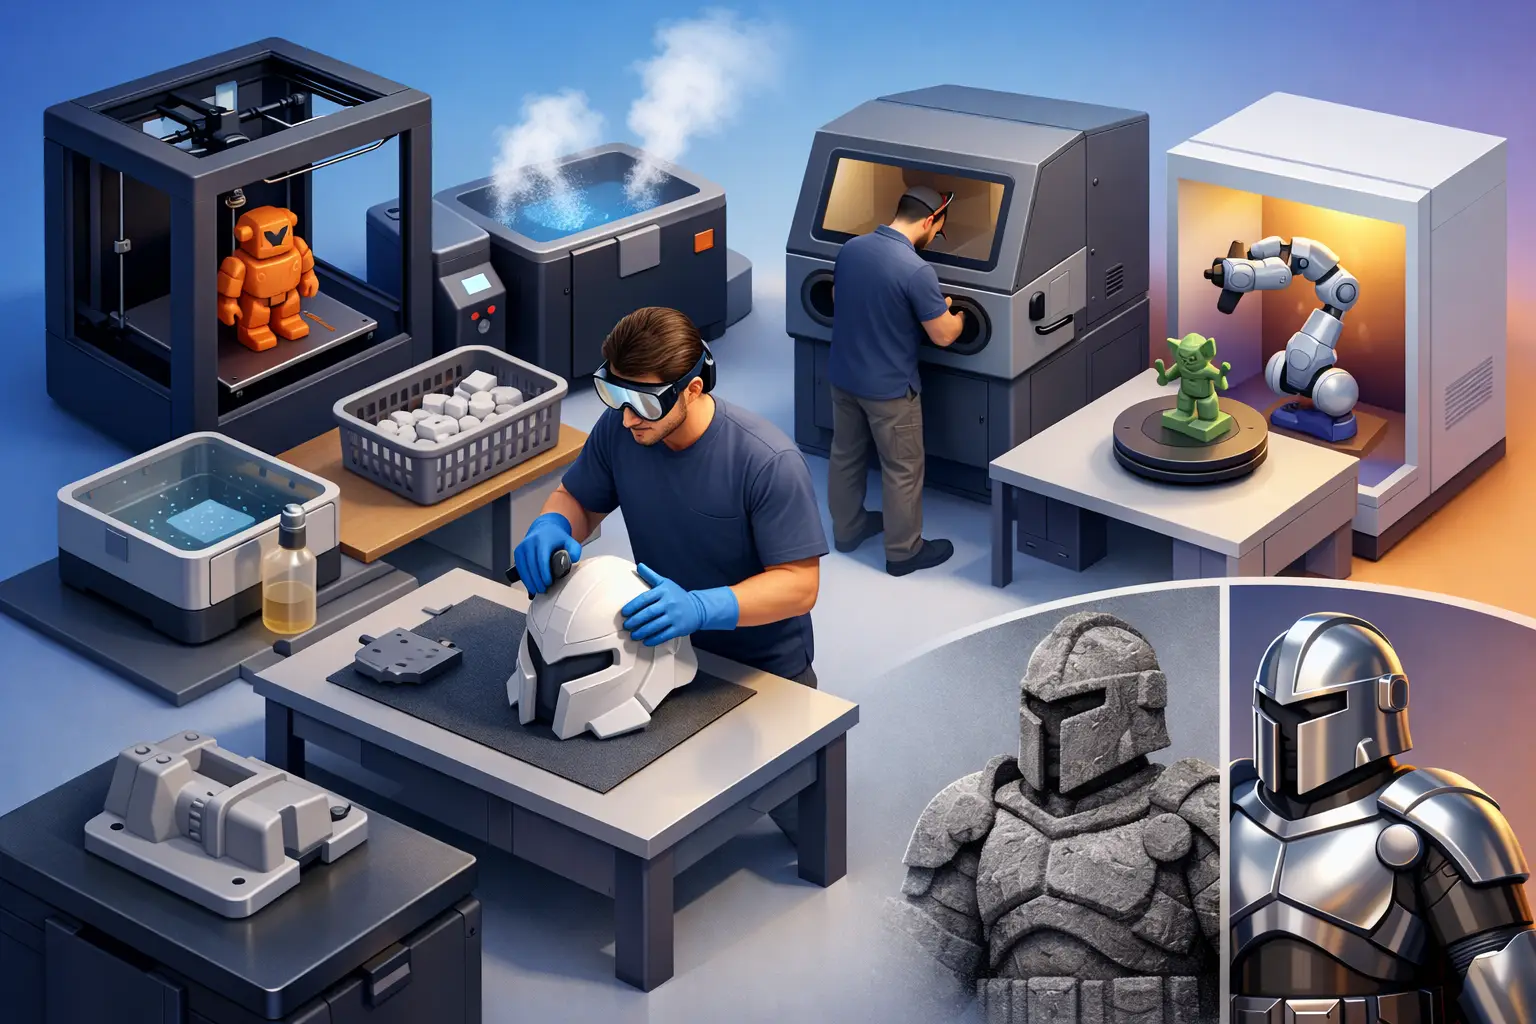
A printed part can leave the machine dimensionally close to the CAD file and still be unready for use. Support structures may block a mating surface, powder may remain in internal channels, or layer texture may be unsuitable for a customer-facing enclosure. The purpose of 3d printing post processing services is to move a part from its as-printed condition to a defined production requirement.
For a prototype, that requirement may be a clean fit check. For an end-use component, it may include controlled surface finish, threaded features, colour, inspection, traceable documentation, and packing for delivery. The correct process depends on the printing technology, material, geometry, quantity, and intended application.
What post processing changes
Post processing is not a single finishing step. It is a sequence of operations selected to address the limitations and advantages of a particular additive manufacturing process. A nylon powder-bed part, a resin part, and a filament-printed fixture do not leave production with the same surface condition, support strategy, or mechanical considerations.
The first operations are often necessary for every order. These can include build removal, support removal, depowdering, washing, and curing. After that, finishing becomes application-specific. A functional bracket may only need light cleanup and hole preparation. A presentation model may require sanding, priming, painting, or a smoother coating system.
Post processing can also affect dimensions. Abrasive finishing removes material. Paint and coatings add material. Thermal operations can introduce small changes depending on the material and geometry. When a part has close-tolerance interfaces, sealing surfaces, snap fits, or bearing locations, those requirements need to be identified before production begins rather than after a print is complete.
Common 3D printing post processing services
Support removal and build cleanup
Many printed parts require supports to hold overhangs, bridges, or complex features during the build. Removing them is a controlled operation, especially where supports contact visible faces or critical dimensions. The goal is to remove support material without damaging thin walls, small details, or functional surfaces.
Build cleanup may also include trimming, removing rafts, clearing loose powder, or cleaning residual resin. These steps sound basic, but they determine whether a part can be handled safely, assembled correctly, or moved to the next finishing stage.
Washing, curing, and depowdering
Photopolymer resin parts are typically washed to remove uncured resin and then post-cured to achieve the required material properties. Cure time and exposure conditions matter because they can affect strength, heat resistance, and final surface quality.
Powder-based parts require thorough depowdering. This is particularly relevant for enclosed volumes, lattice structures, and internal passages. If the design includes channels or cavities, provide their intended function and any access constraints. A channel designed for fluid or air flow needs different verification from a decorative hollow feature.
Sanding, bead blasting, and surface refinement
Abrasive finishing reduces visible layer texture, blends support-contact areas, and creates a more consistent appearance. Sanding is often used where a smoother surface is required before painting or coating. Bead blasting can produce an even matte finish on suitable materials and geometries.
These methods are useful, but they are not neutral. Edges can soften, fine text can lose definition, and tight external dimensions can change. Specify cosmetic zones and critical zones separately where possible. A part may need a refined exterior face while retaining untouched datum surfaces for assembly.
Painting, dyeing, and protective coatings
Colour can be selected during material configuration, but post-process colouring provides additional control where a printed material does not offer the required appearance. Dyeing may suit certain polymers, while painting can support colour matching, visual differentiation, or a presentation-grade finish.
Coatings may improve appearance, reduce surface porosity, or provide a more uniform feel. They also introduce process variables: masking, cure time, coating thickness, adhesion, and durability under handling. If a component will be exposed to heat, cleaning agents, UV light, abrasion, or repeated contact, identify those conditions before a coating is selected.
Machining, inserts, and assembly preparation
Additive manufacturing is often most effective when it is combined with conventional finishing. Holes may be drilled or reamed to size. Threads may be tapped, or heat-set and threaded inserts may be installed to support repeated fastening. Mating faces can be machined where a printed surface alone does not meet the fit requirement.
This approach is common for jigs, fixtures, enclosures, test components, and low-volume production parts. It allows the printed geometry to carry the complex shape while conventional operations establish the features that need greater precision or wear resistance.
Specify the result, not only the process
A request for a part to be “smooth” or “finished” leaves too much open to interpretation. Useful order information describes the functional result. State whether the part is for visual review, a one-time assembly, repeated field use, or a customer-facing product. Identify which surfaces are visible and which dimensions control fit.
For example, a prototype enclosure may need supports removed, light sanding on exterior faces, and threaded inserts at mounting points. A powder-bed nylon duct may need full depowdering, cleaning of airflow passages, and inspection of connection geometry. A fixture may need only support removal and reamed alignment holes. Each is a different post-processing plan, even if the parts have similar overall size.
Where available, use drawings, annotated renders, or CAD notes to identify no-finish areas, masked areas, thread specifications, cosmetic faces, and acceptable surface condition. Include tolerances only where they are necessary. Applying close tolerances to every feature can increase cost and lead time without improving the function of the part.
Plan for material and technology limits
The post-processing method must suit the selected material. A rigid resin can produce fine detail but may require careful support removal to avoid damage. Flexible materials can be harder to sand cleanly. Fibre-filled polymers may machine differently from unfilled grades. Powder-based polymers generally have a characteristic texture that can be refined, but not every geometry is suitable for aggressive surface work.
Part design also affects process access. Deep recesses, narrow gaps, internal channels, thin features, and sharp corners can limit blasting, sanding, coating, or support removal. If the part must be coated internally or cleaned through a narrow opening, raise the requirement before ordering. In some cases, a small design revision, such as an access hole or a different build orientation, produces a better and more predictable result.
Quantity changes the decision as well. A hand-finished single prototype may be appropriate for design review. For repeat orders, a defined and repeatable finish is usually more valuable than a highly variable manual process. Teams should document approved finishing requirements alongside the material, colour, technology, and revision level.
Inspection and order control matter
Post processing should be connected to an order record, not treated as an informal request after production starts. The order should capture the selected finish, required inserts or machining, certification needs, delivery method, and any inspection criteria. This creates a reference point for production teams and purchasing stakeholders.
Inspection can be visual, dimensional, or functional. Visual inspection checks finish consistency, support marks, colour, and obvious defects. Dimensional inspection focuses on the features that affect assembly. Functional inspection may confirm that a lid closes, a thread accepts the intended fastener, or a channel remains clear after finishing.
For teams managing several parts or repeat builds, centralized tracking reduces confusion between revisions and finish instructions. Print3Dcanada supports configurable order details and production status tracking so material, post-processing, charges, and fulfilment information remain tied to the same workflow.
When to use a lighter finish
More finishing is not always better. An as-printed or lightly cleaned surface can be the right choice for early prototypes, concealed brackets, production aids, and parts where speed or cost takes priority over appearance. A lighter finish also preserves more of the original printed geometry.
Use a higher level of finishing when the part will be handled frequently, presented to stakeholders, installed in a visible location, or used in an assembly with defined interface requirements. The practical decision is based on what the part must do, what users will see, and which features cannot be compromised.
A clear post-processing requirement gives a production team something actionable: the material, the selected technology, the surfaces that matter, the operations required, and the acceptance standard. Define those details at the order stage, and the finished part is far more likely to arrive ready for its intended next step.